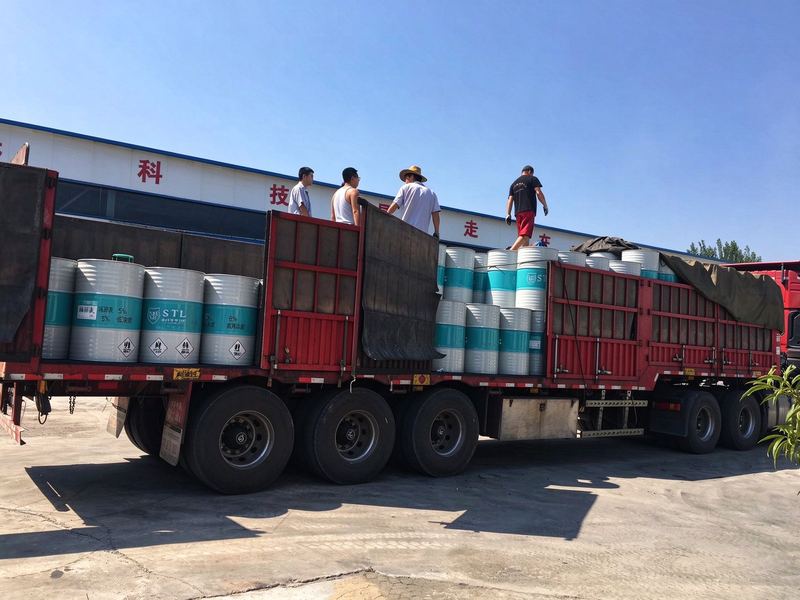
| Fully synthetic cutting fluid | Cast iron, low-alloy steel — turning, milling, surface grinding | pH 9.3 @ 5 % · cast-iron rust pass | 20 / 200 L |
| Environmentally friendly synthetic cutting fluid | Aluminium and its alloys — cutting, drilling, milling | pH 9.0 @ 5 % · aluminium corrosion pass | 20 / 200 L |
| Synthetic grinding fluid | Ferrous grinding — protects the wheel, controls heat | pH 9.5 @ 5 % · cast-iron rust pass | 20 / 200 L |
| Rust-proof emulsion cutting fluid | Iron, aluminium, alloy steel — turning, tapping, milling | pH 9.0 @ 5 % · 4 % rust pass · 3 % Al pass | 20 / 200 L |
| Rust-proof emulsified oil | Iron, aluminium, alloy steel — general machining | pH 9.0 @ 5 % · 4 % rust pass | 20 / 200 L |
| Extreme-pressure rust-proof emulsified oil | Iron, aluminium, alloy steel — heavier cuts | pH 9.0 @ 5 % · rust and Al pass | 20 / 200 L |
| Water-soluble drawing oil | Copper and aluminium wire — coarse, medium and fine drawing | pH 8.6 @ 5 % · milky dilution · Cu/Al pass | 20 / 200 L |
| Water-soluble cutting fluid | Cast iron and steel — cutting, milling, surface grinding | pH 9.2 @ 5 % · 4 % rust pass | 20 / 200 L |
| Extreme-pressure tapping oil (neat) | Tapping and threading — high-pressure contact | Near odourless · low mist · SG > 0.8 | 20 / 200 L |
| Synthetic wire EDM fluid | Ferrous and non-ferrous — 1xxx–7xxx aluminium, stainless, copper | pH 9.6 ± 0.5 @ 5 % · copper strip 1a | 20 / 200 L |
| Cold-heading forming oil (neat) | Stainless bolts, nuts, rivets — multi-station cold forming | 110–120 mm²/s @ 40 °C · flash ≥ 180 °C | 20 / 200 L |
| High-temperature lithium grease | High-speed, high-temperature and low-temperature bearings | Drop point 316 °C · evaporation 2.66 % @ 200 °C | 20 / 200 L |